Who we are.
Alamir Ingredients is the newest strategic business unit launched under Alamir Group, with the vision of becoming one of Egypt’s leading manufacturers and exporters of premium tomato concentrates, fruit concentrates and fruit purees for the global food and beverage industry.
Extending a story that began in 1970.
Alamir Ingredients extends the heritage of Al Amir Group, which began in 1970 and has since reached over 120,000 MT of exports — pulses, sesame, tahini, spices, dates and raisins — to buyers in more than 60 countries across Europe, the GCC, North Africa and the Far East. The Group also imports over 100,000 metric tonnes annually of pulses, green coffee beans, nuts, dried fruits and spice commodities for the Egyptian domestic market.
Alamir Ingredients operates exclusively within the business-to-business sector, supplying food manufacturers, beverage producers, dairy companies, confectionery manufacturers, sauce producers and industrial processors with high-quality fruit and vegetable ingredients.
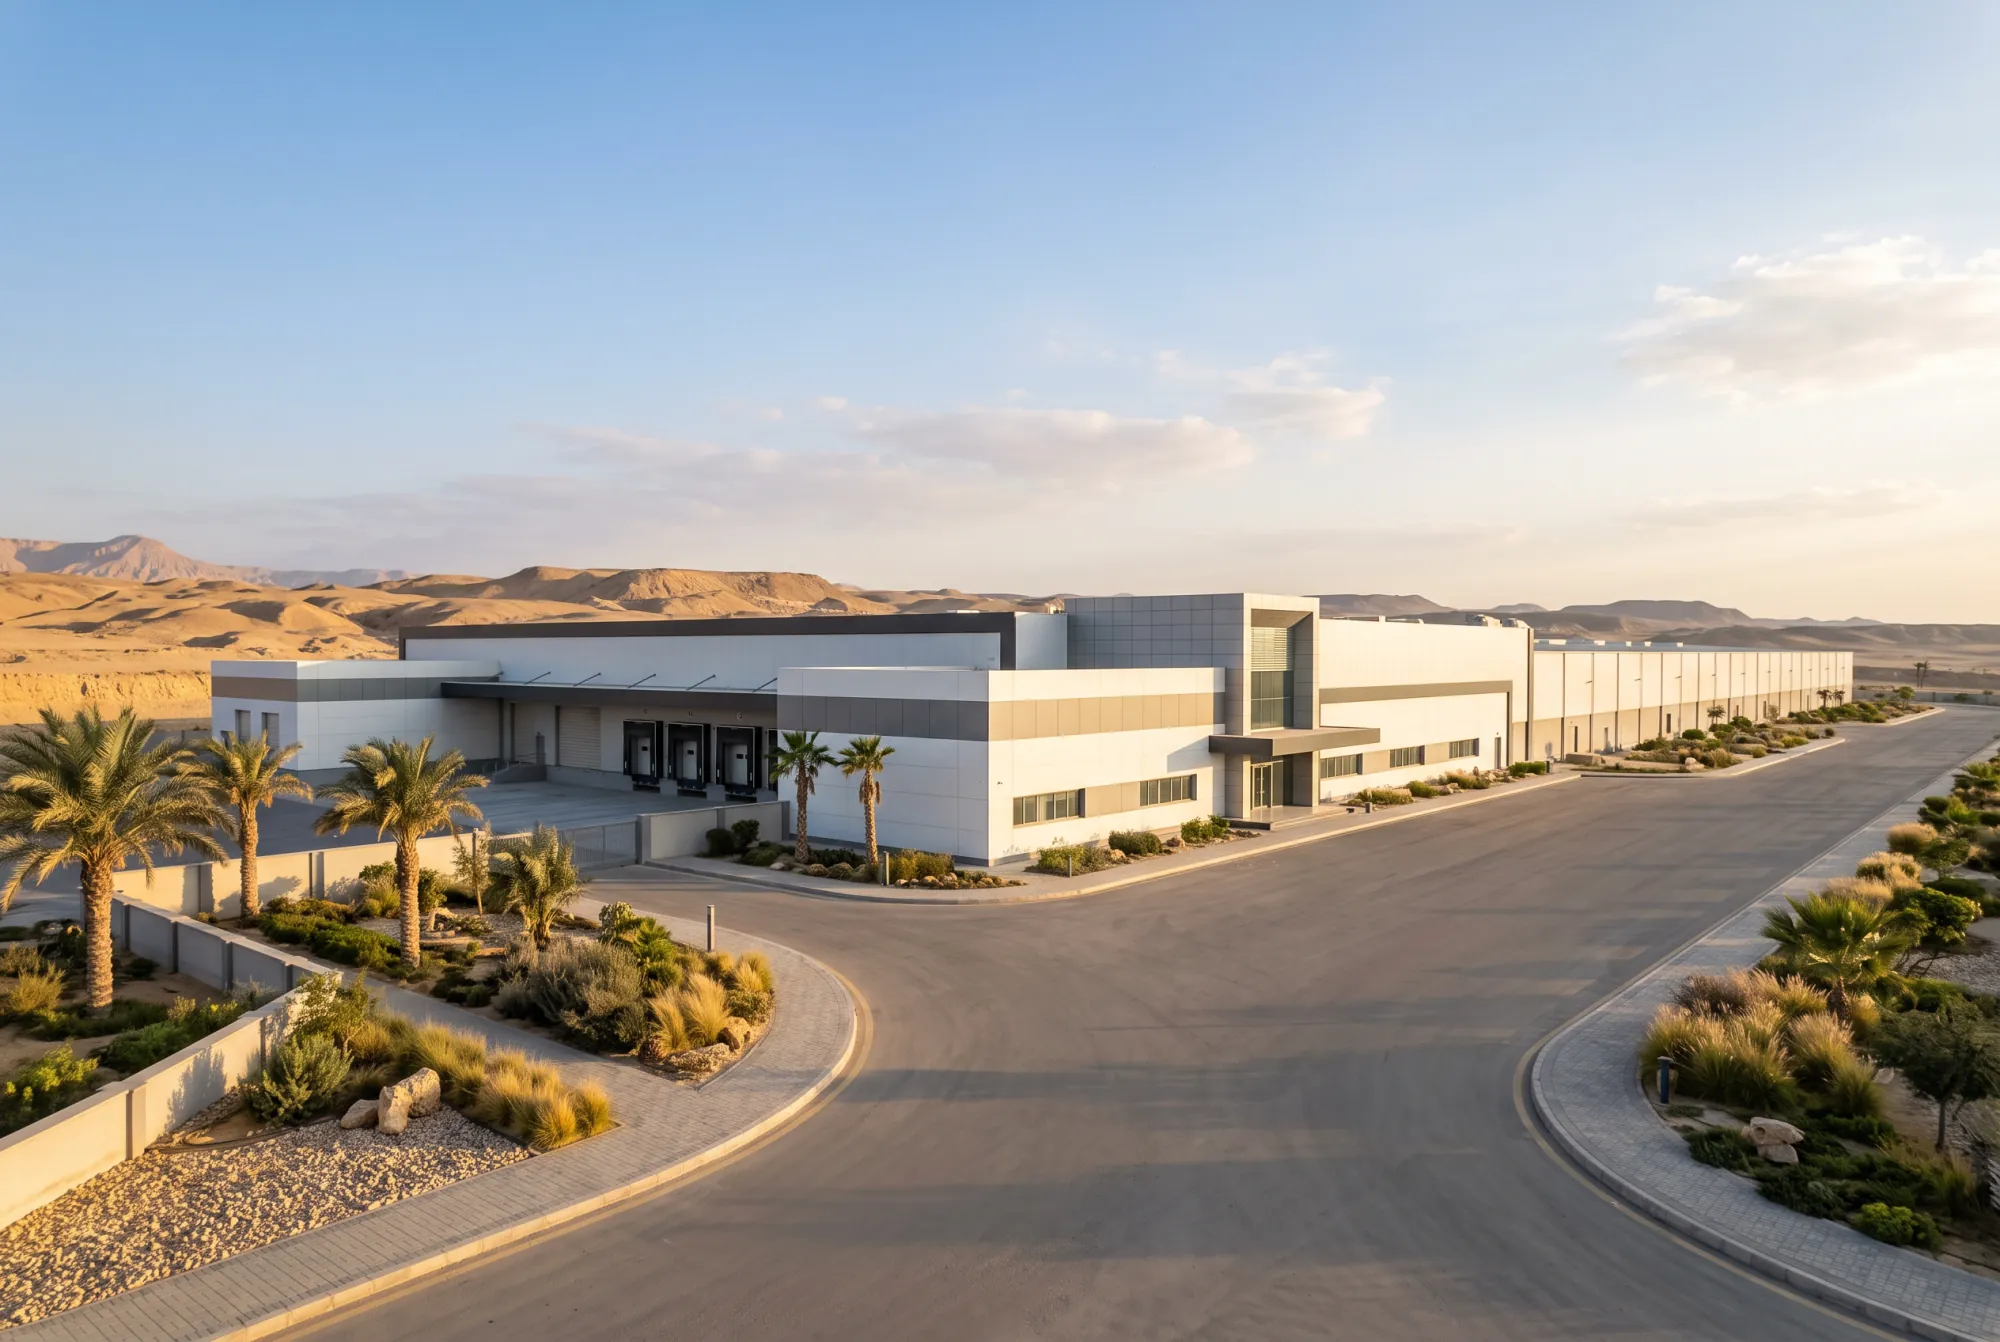
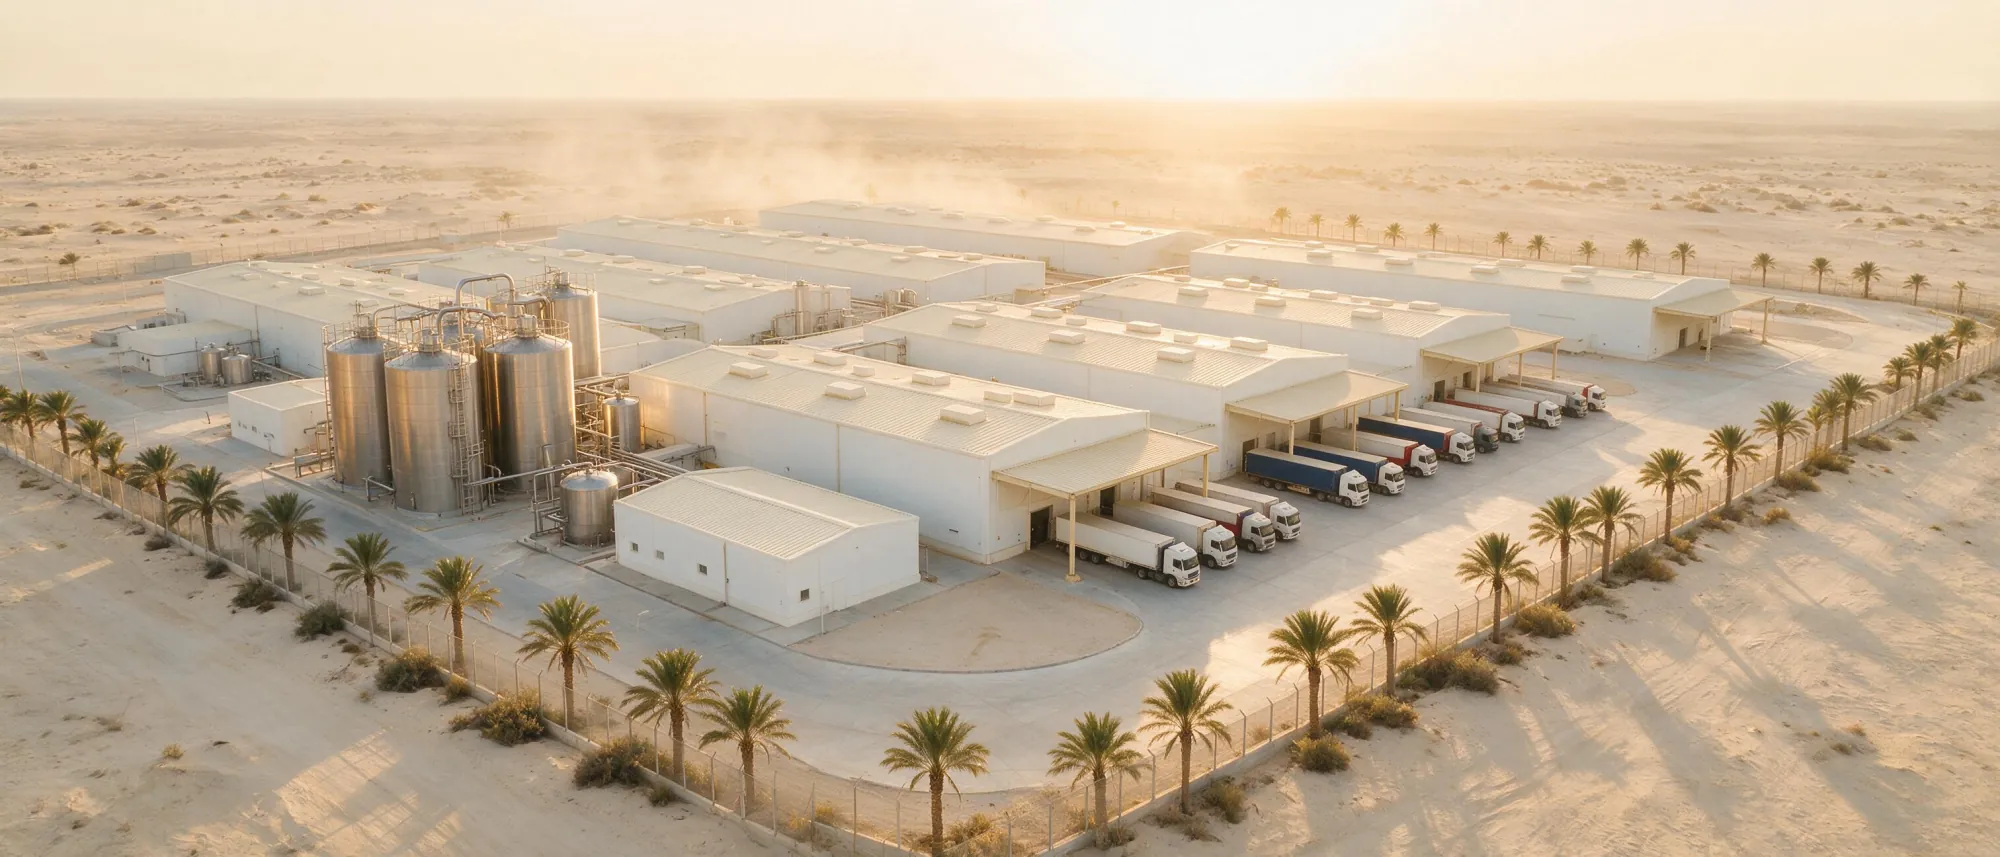
Strategically located in Sadat City, the manufacturing facility spans 37,660 sqm with direct access to agricultural supply chains, transportation infrastructure and export logistics, allowing the company to serve both domestic and international markets efficiently.
Alamir Ingredients is positioned as an industrial ingredient partner that enables manufacturers to produce high-quality products through reliable sourcing, consistent quality and customised ingredient solutions.
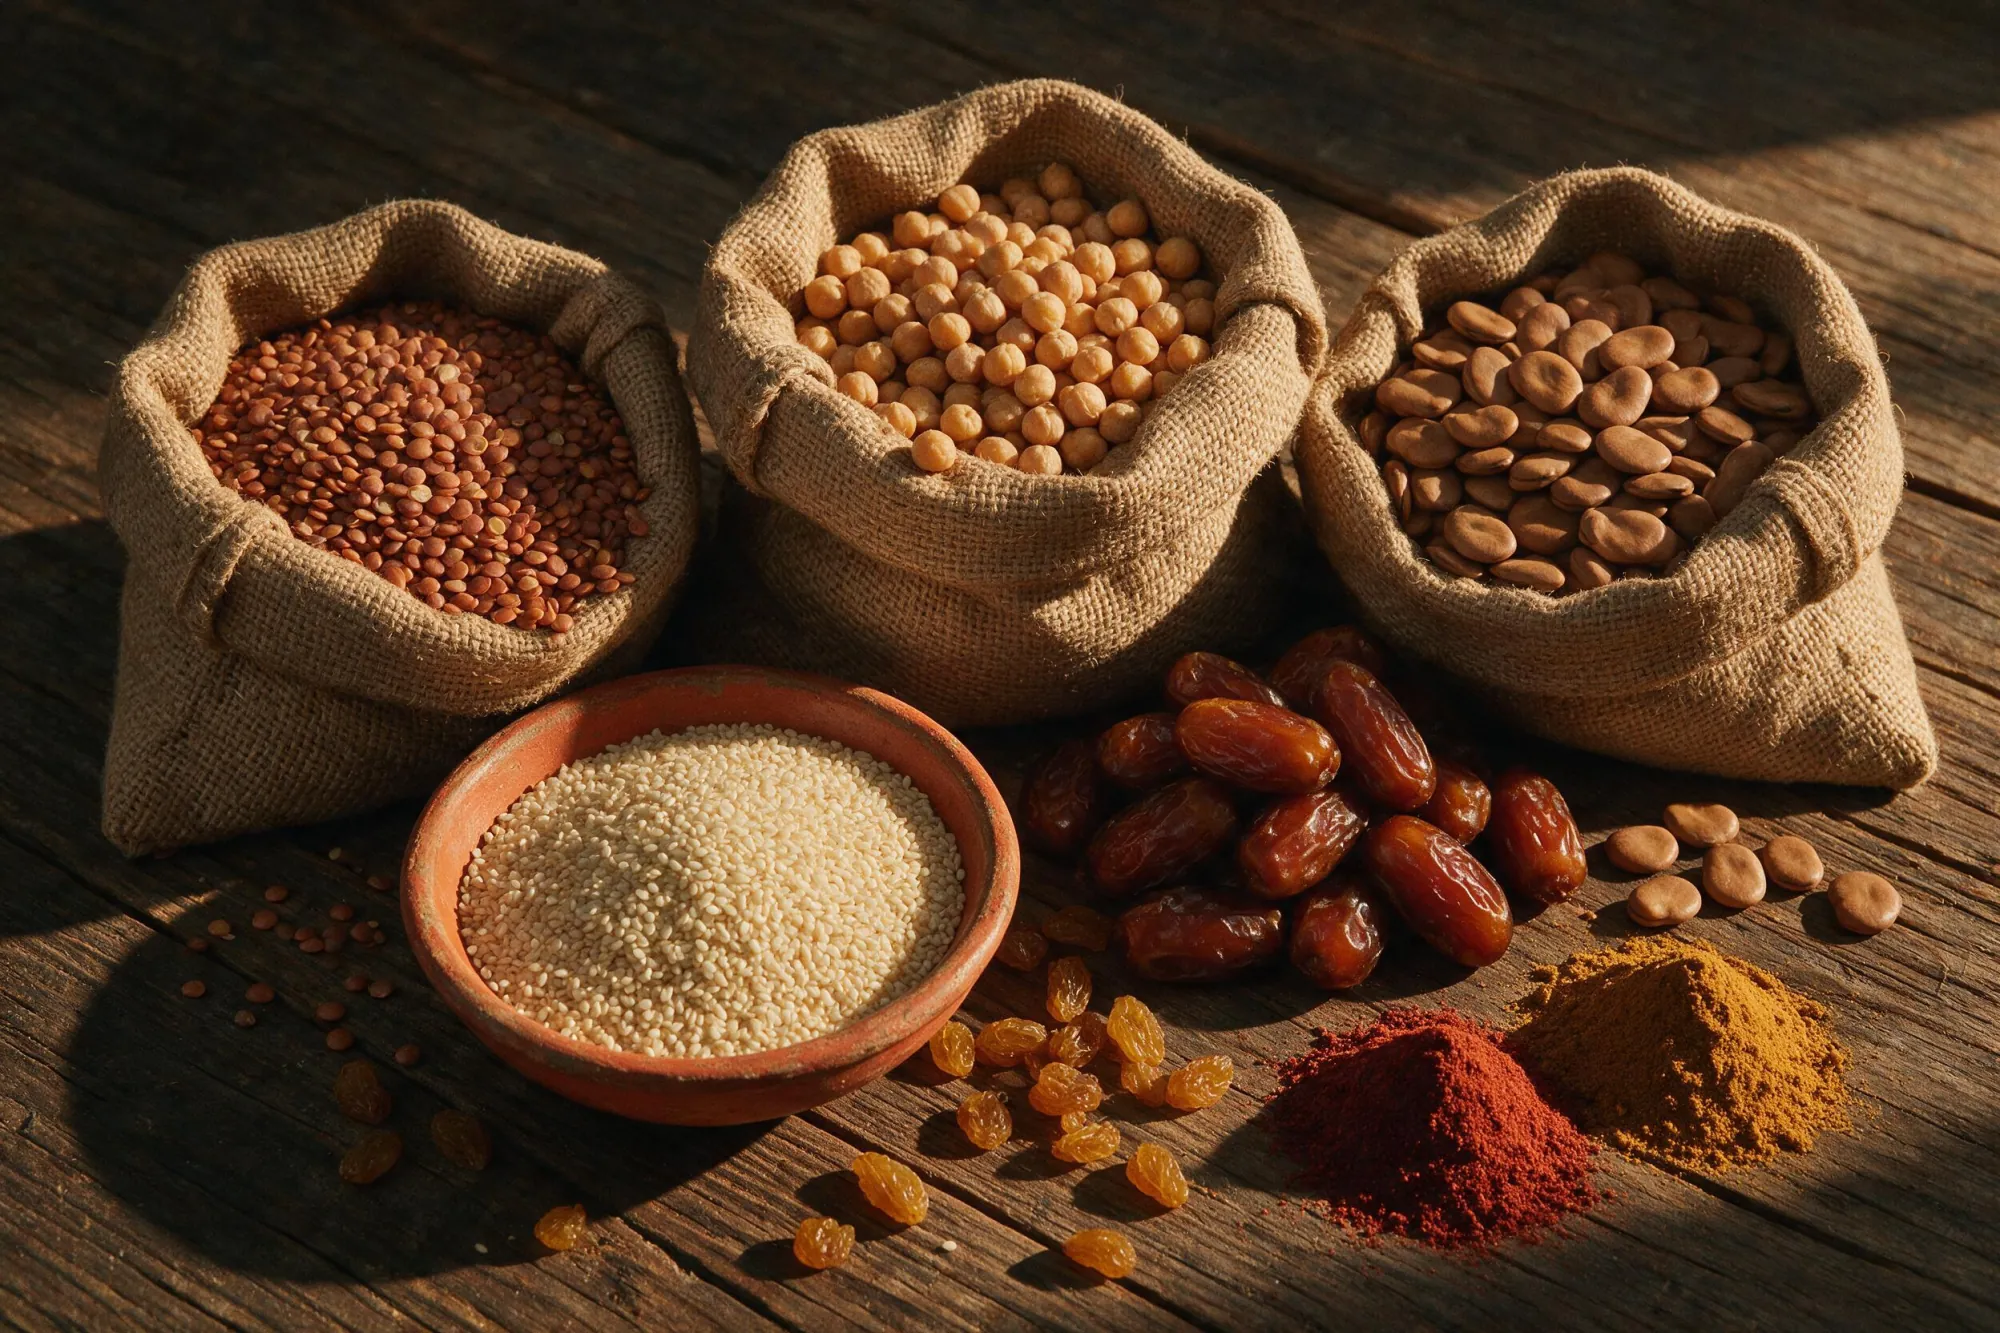
Pulses, sesame, spices, dates.
Fifty-five years of moving agricultural commodities to more than sixty countries taught the Group the part buyers actually care about: that the second shipment matches the first.
Where we are going, and how.
A fifty-five-year trading heritage, taken into manufacturing and held to a specification. The vision sets where this goes; the mission is what it costs to get there.
Alamir Ingredients extends the heritage of Al Amir Group, which began in 1970 and has since reached over sixty export markets across four regions.
Empowering food manufacturers worldwide — concentrates and purees powered by advanced technology, uncompromised quality and trusted partnerships, through satisfied teams.
To be the benchmark for food & beverage ingredients.
What we stand on.
-
01
Quality excellence
Maintaining traceability and stable quality for every batch through high standards, precision and continuous quality certification — from field to sealed pack.
-
02
Partnership
Building trusted, long-term relationships based on collaboration and mutual success, because the second shipment matters more than the first.
-
03
Accountability
Honouring every commitment through reliability and consistency — on time, on spec, with dependable customer service.
-
04
Innovation & technology
Driving progress through advanced Italian CFT technologies engineered for consistency at industrial scale, with full aseptic control.
-
05
Empowerment
Empowering our people to perform at their best while enabling our customers to achieve lasting success.
-
06
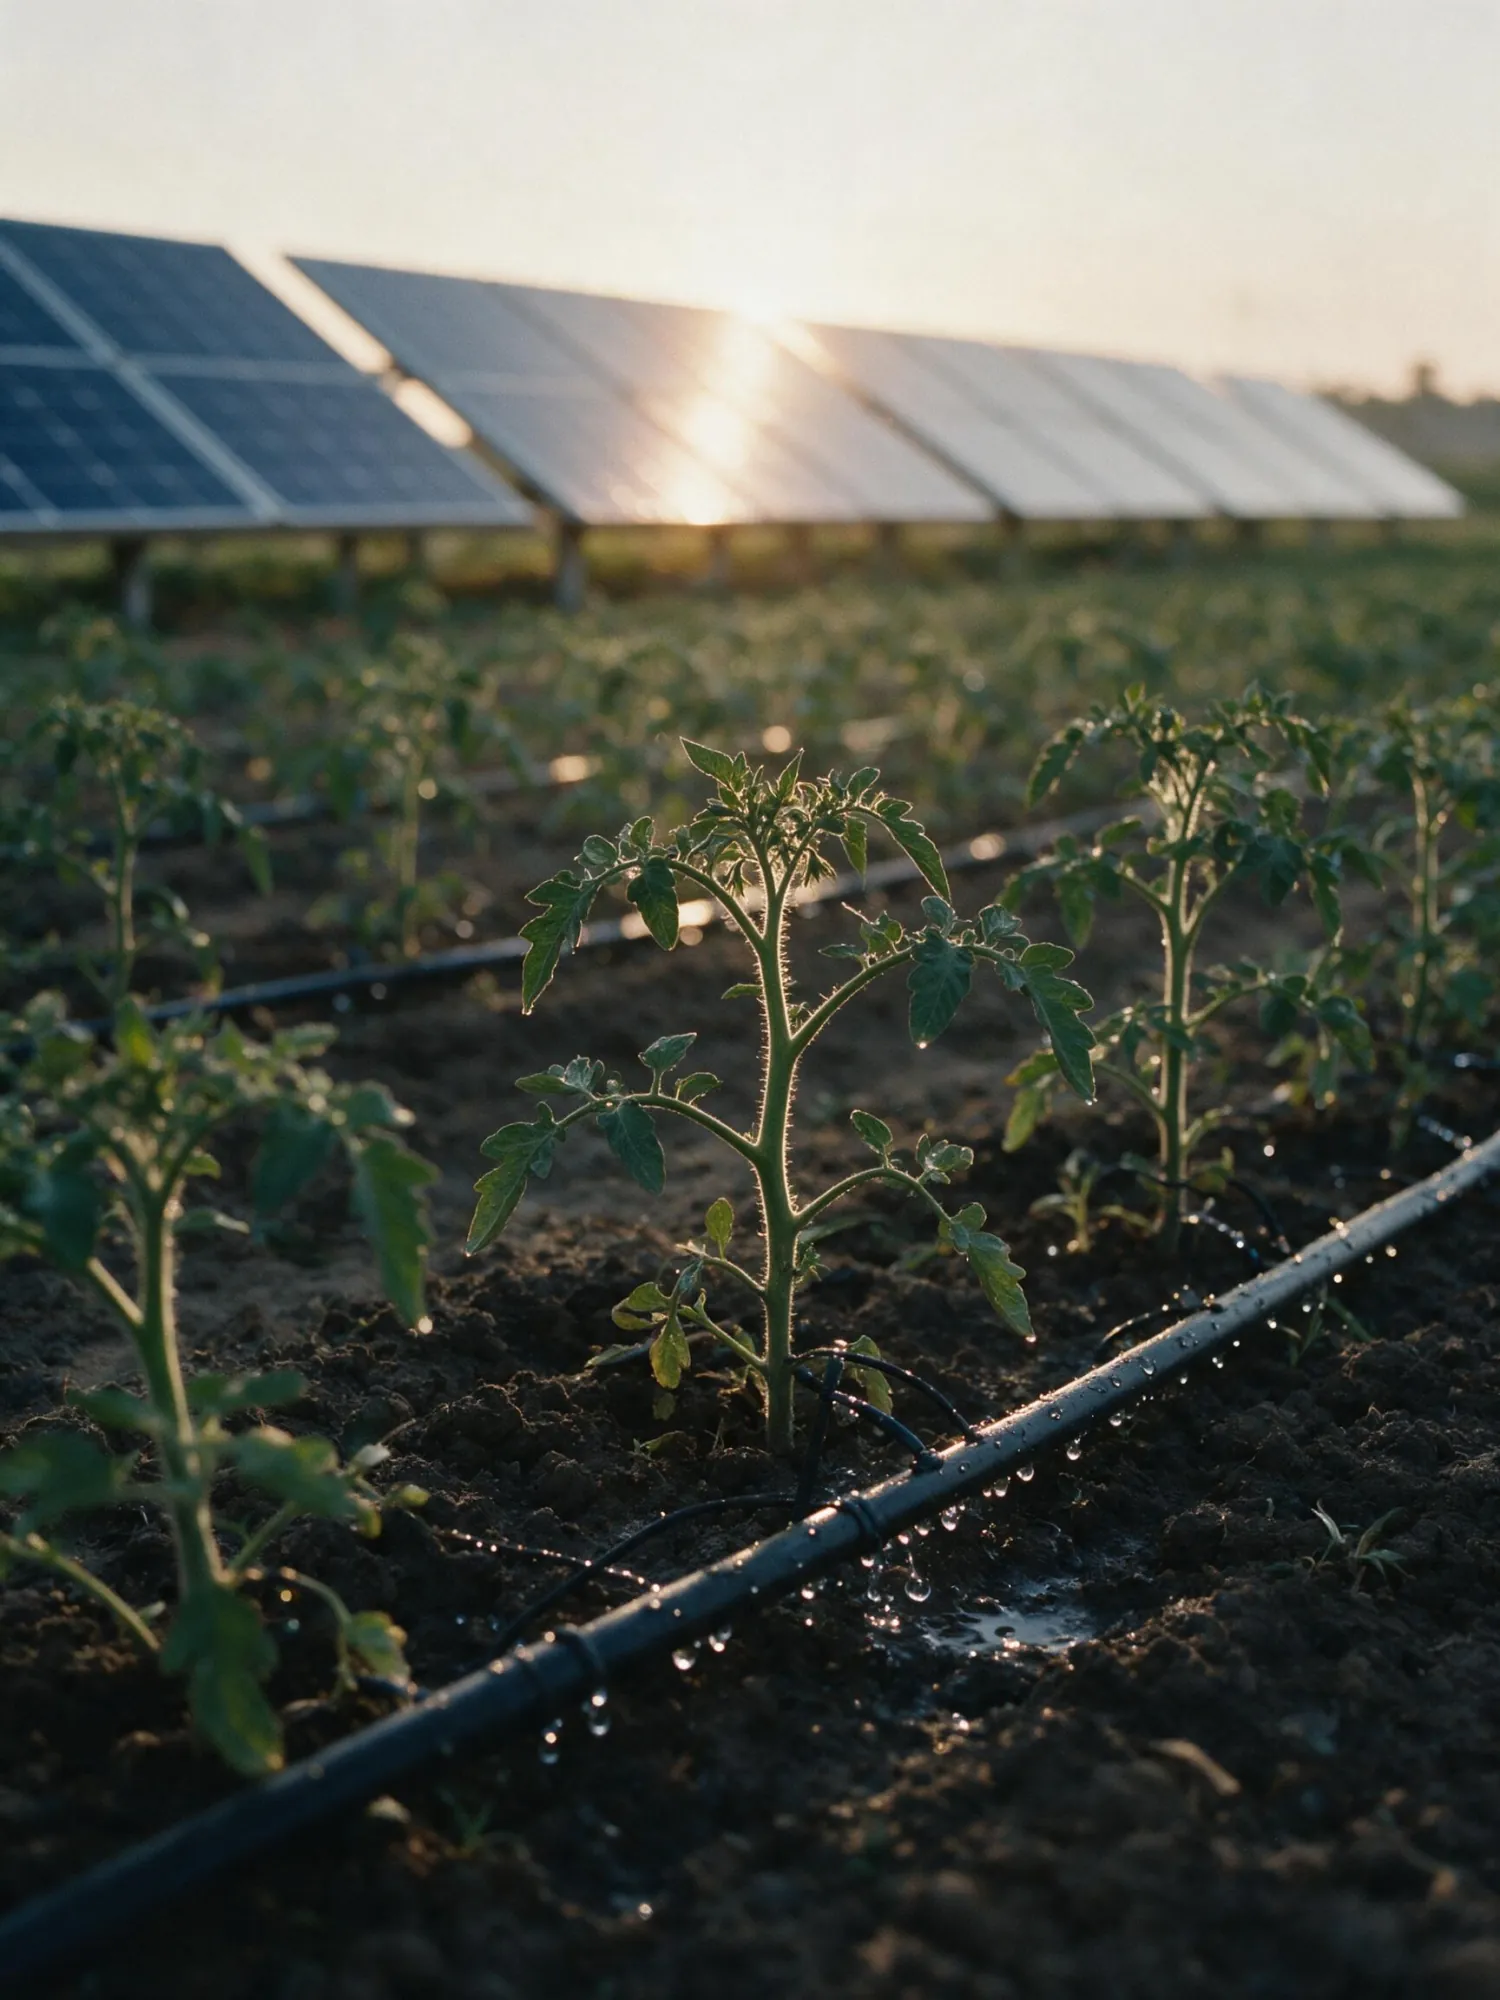
Sustainability
Creating lasting value through responsible practices and the efficient use of resources.
CFT technology, aseptic from field to drum.
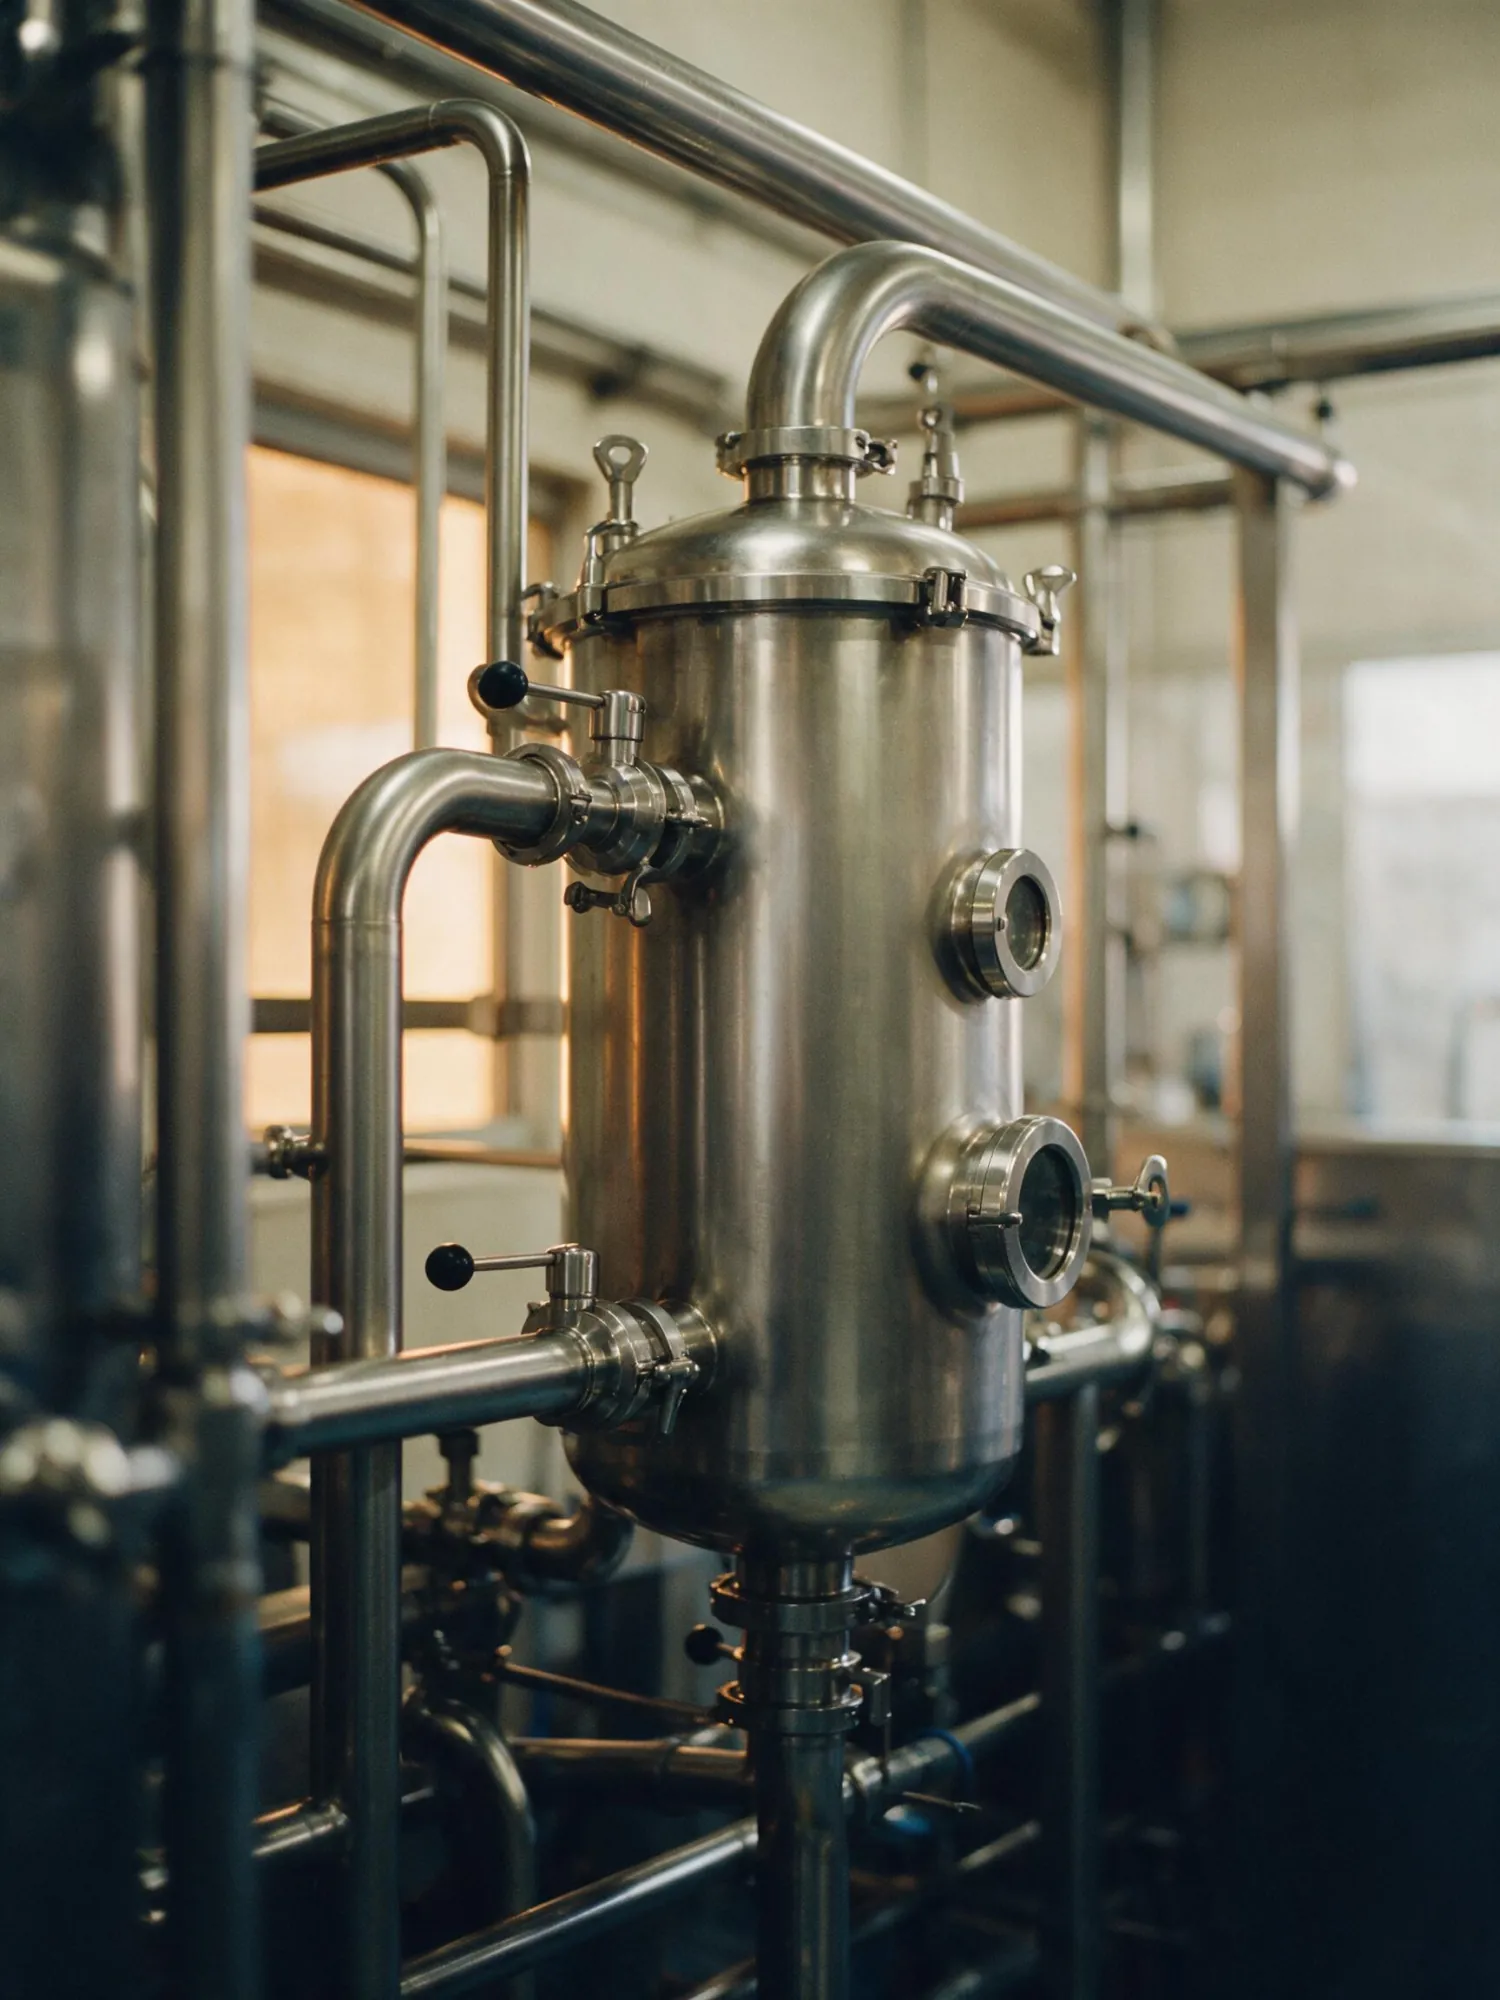
Our concentrates and purees are processed with Italian technology. Powered by advanced CFT processing, our fully automated production line handles up to 900 tonnes of tomatoes and 240 tonnes of tropical fruits per day, ensuring exceptional efficiency and consistency.
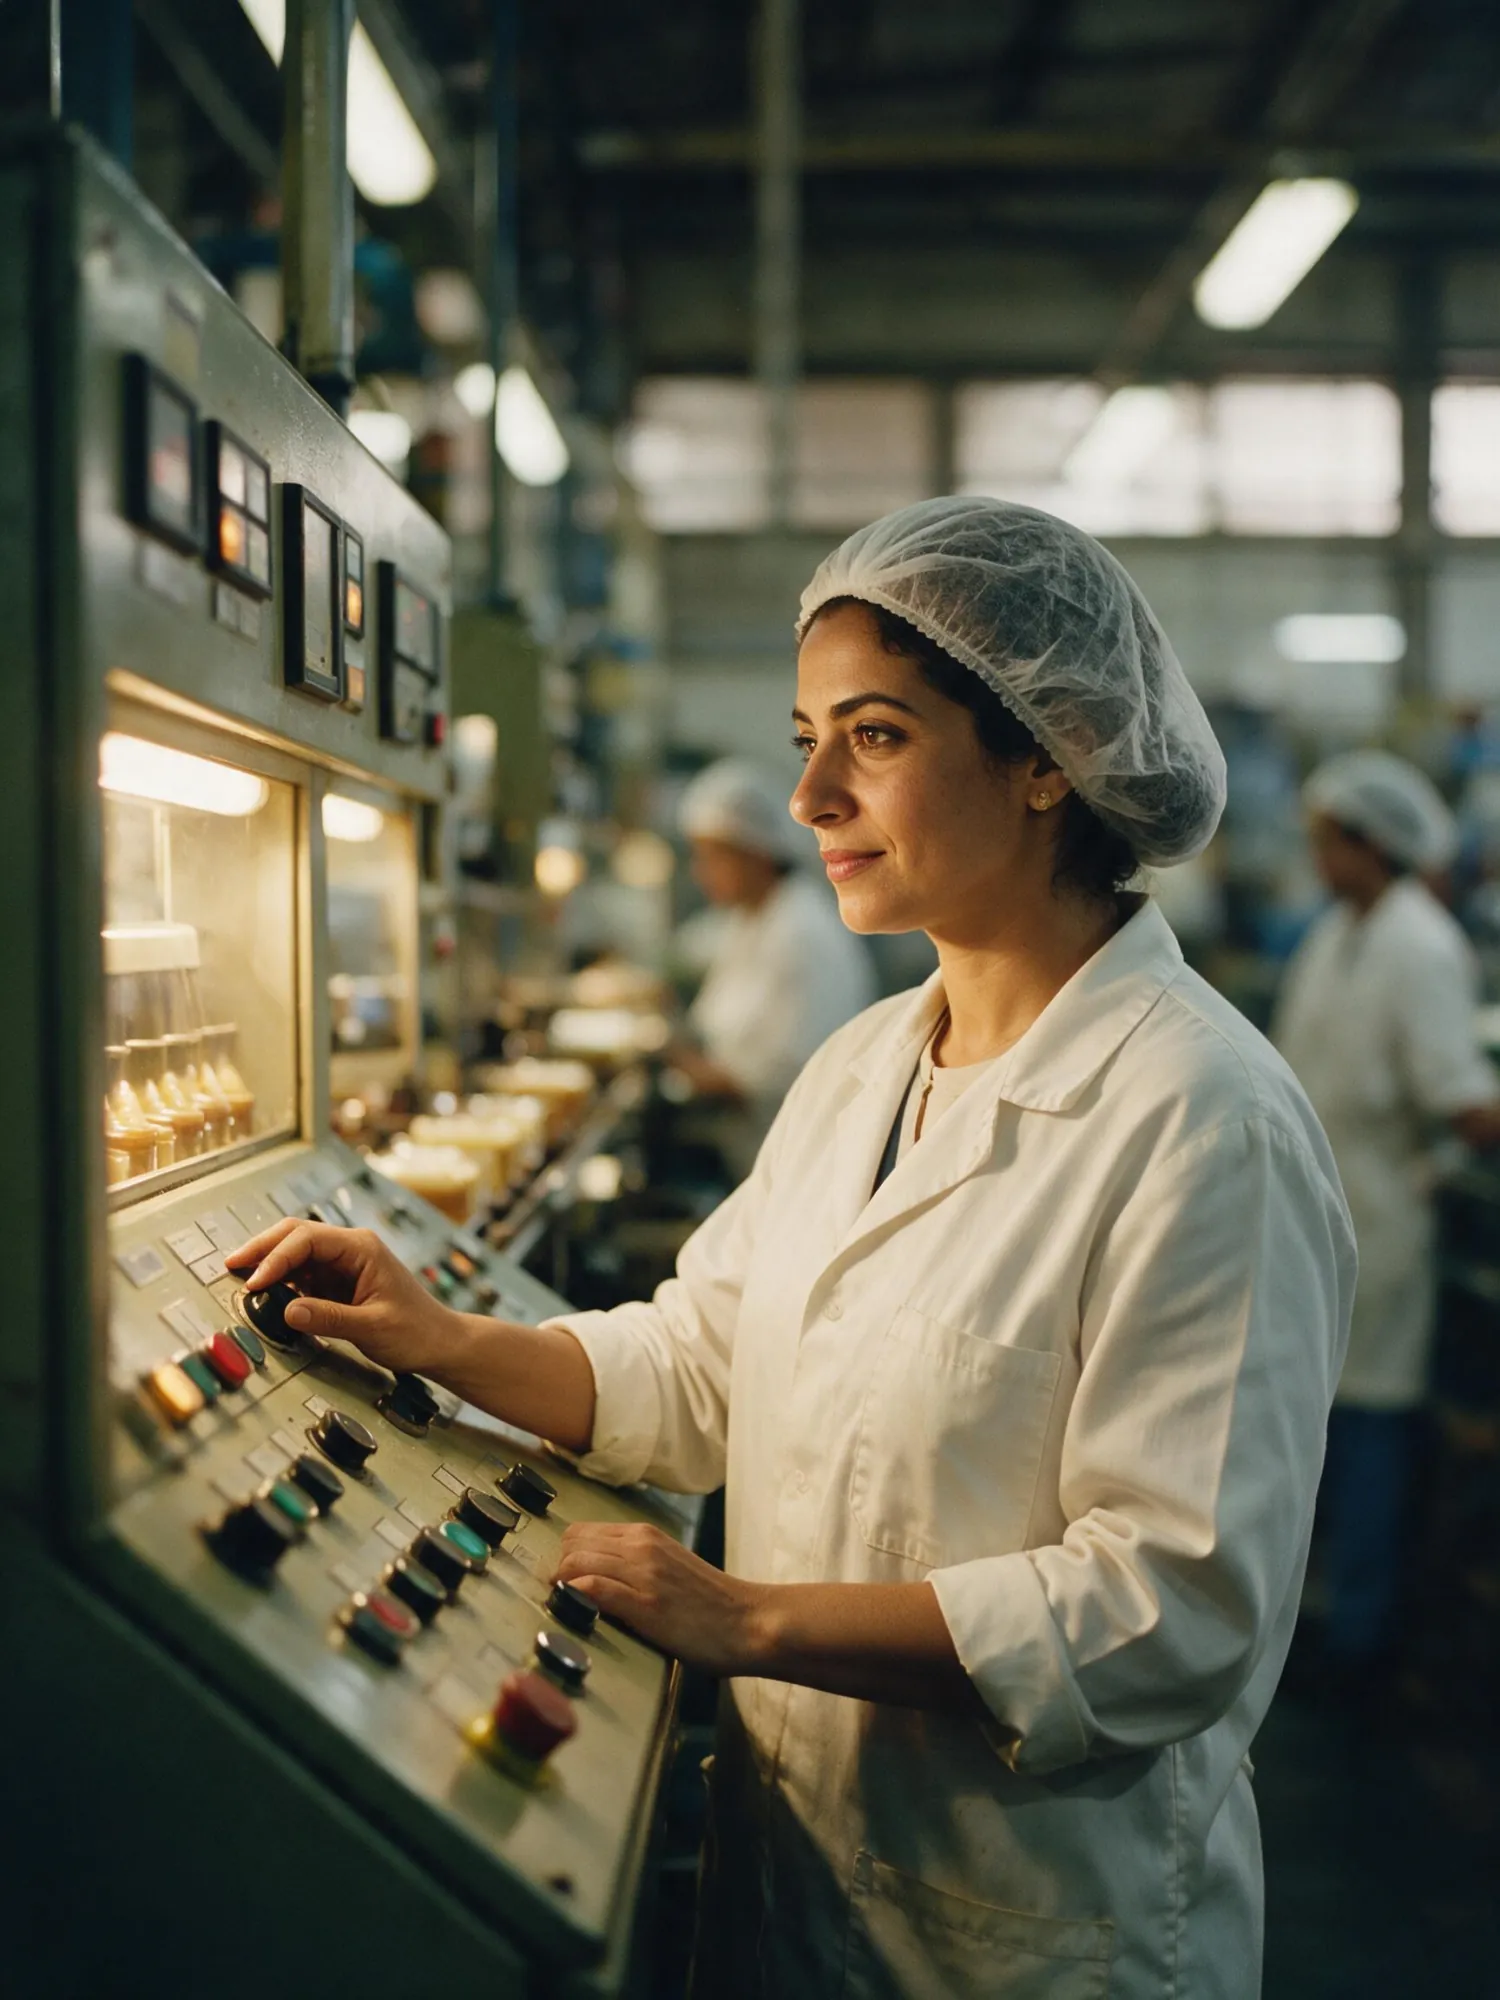
Patented cold extraction, vacuum concentration and aseptic filling technologies preserve the natural flavour, colour and nutritional value of every product while meeting the highest international food safety standards. Intelligent PLC-controlled automation and advanced aseptic processing deliver premium-quality concentrates with maximum reliability and traceability.
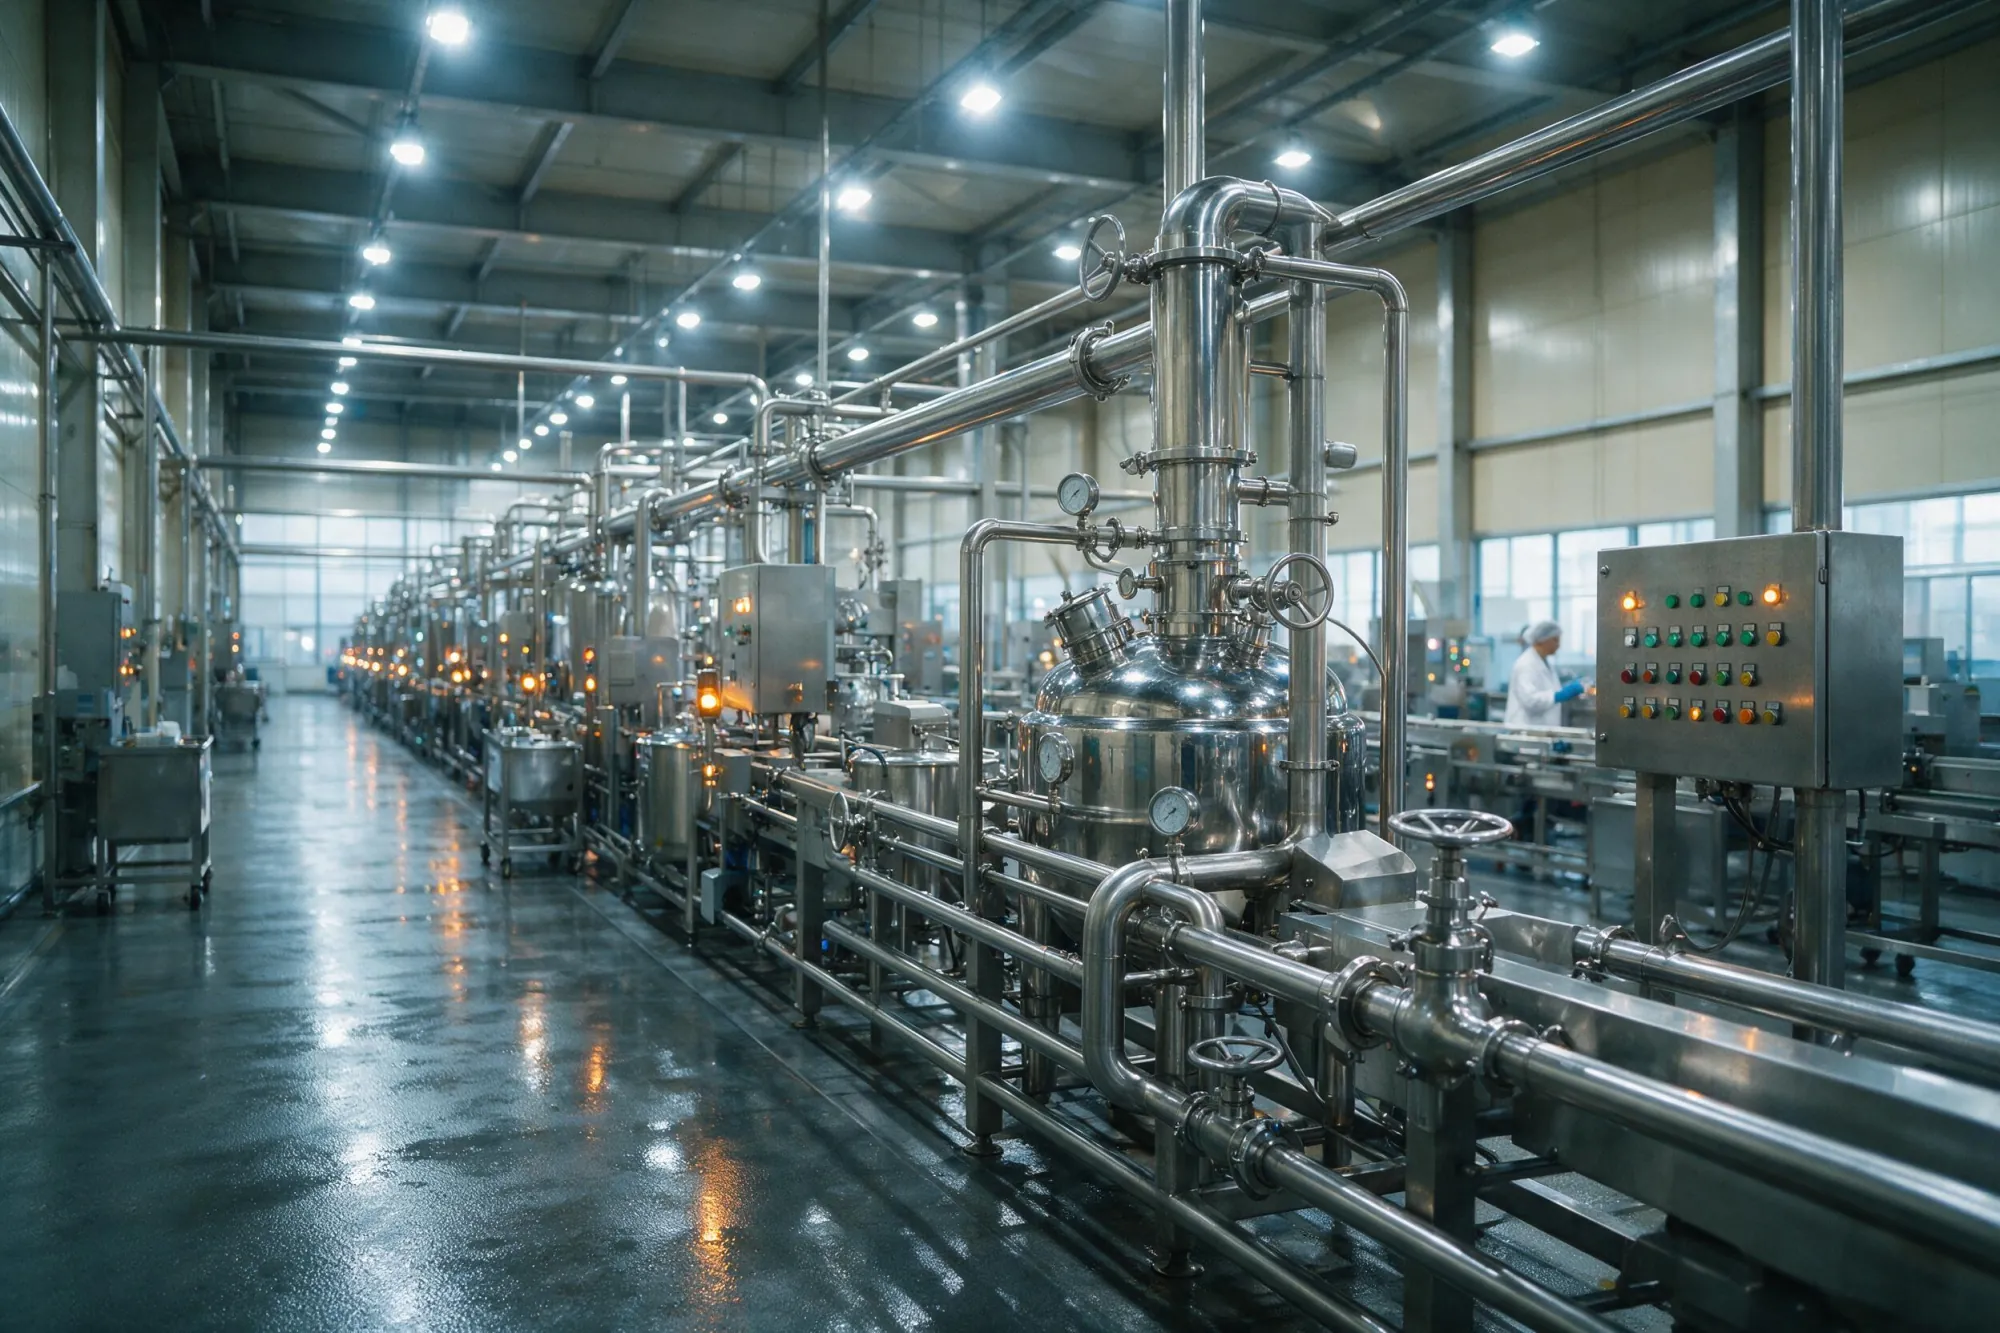
900 tonnes of tomatoes a day.
Cold extraction and vacuum concentration, PLC-controlled end to end. The line also takes 240 tonnes of tropical fruit a day without changing hands.
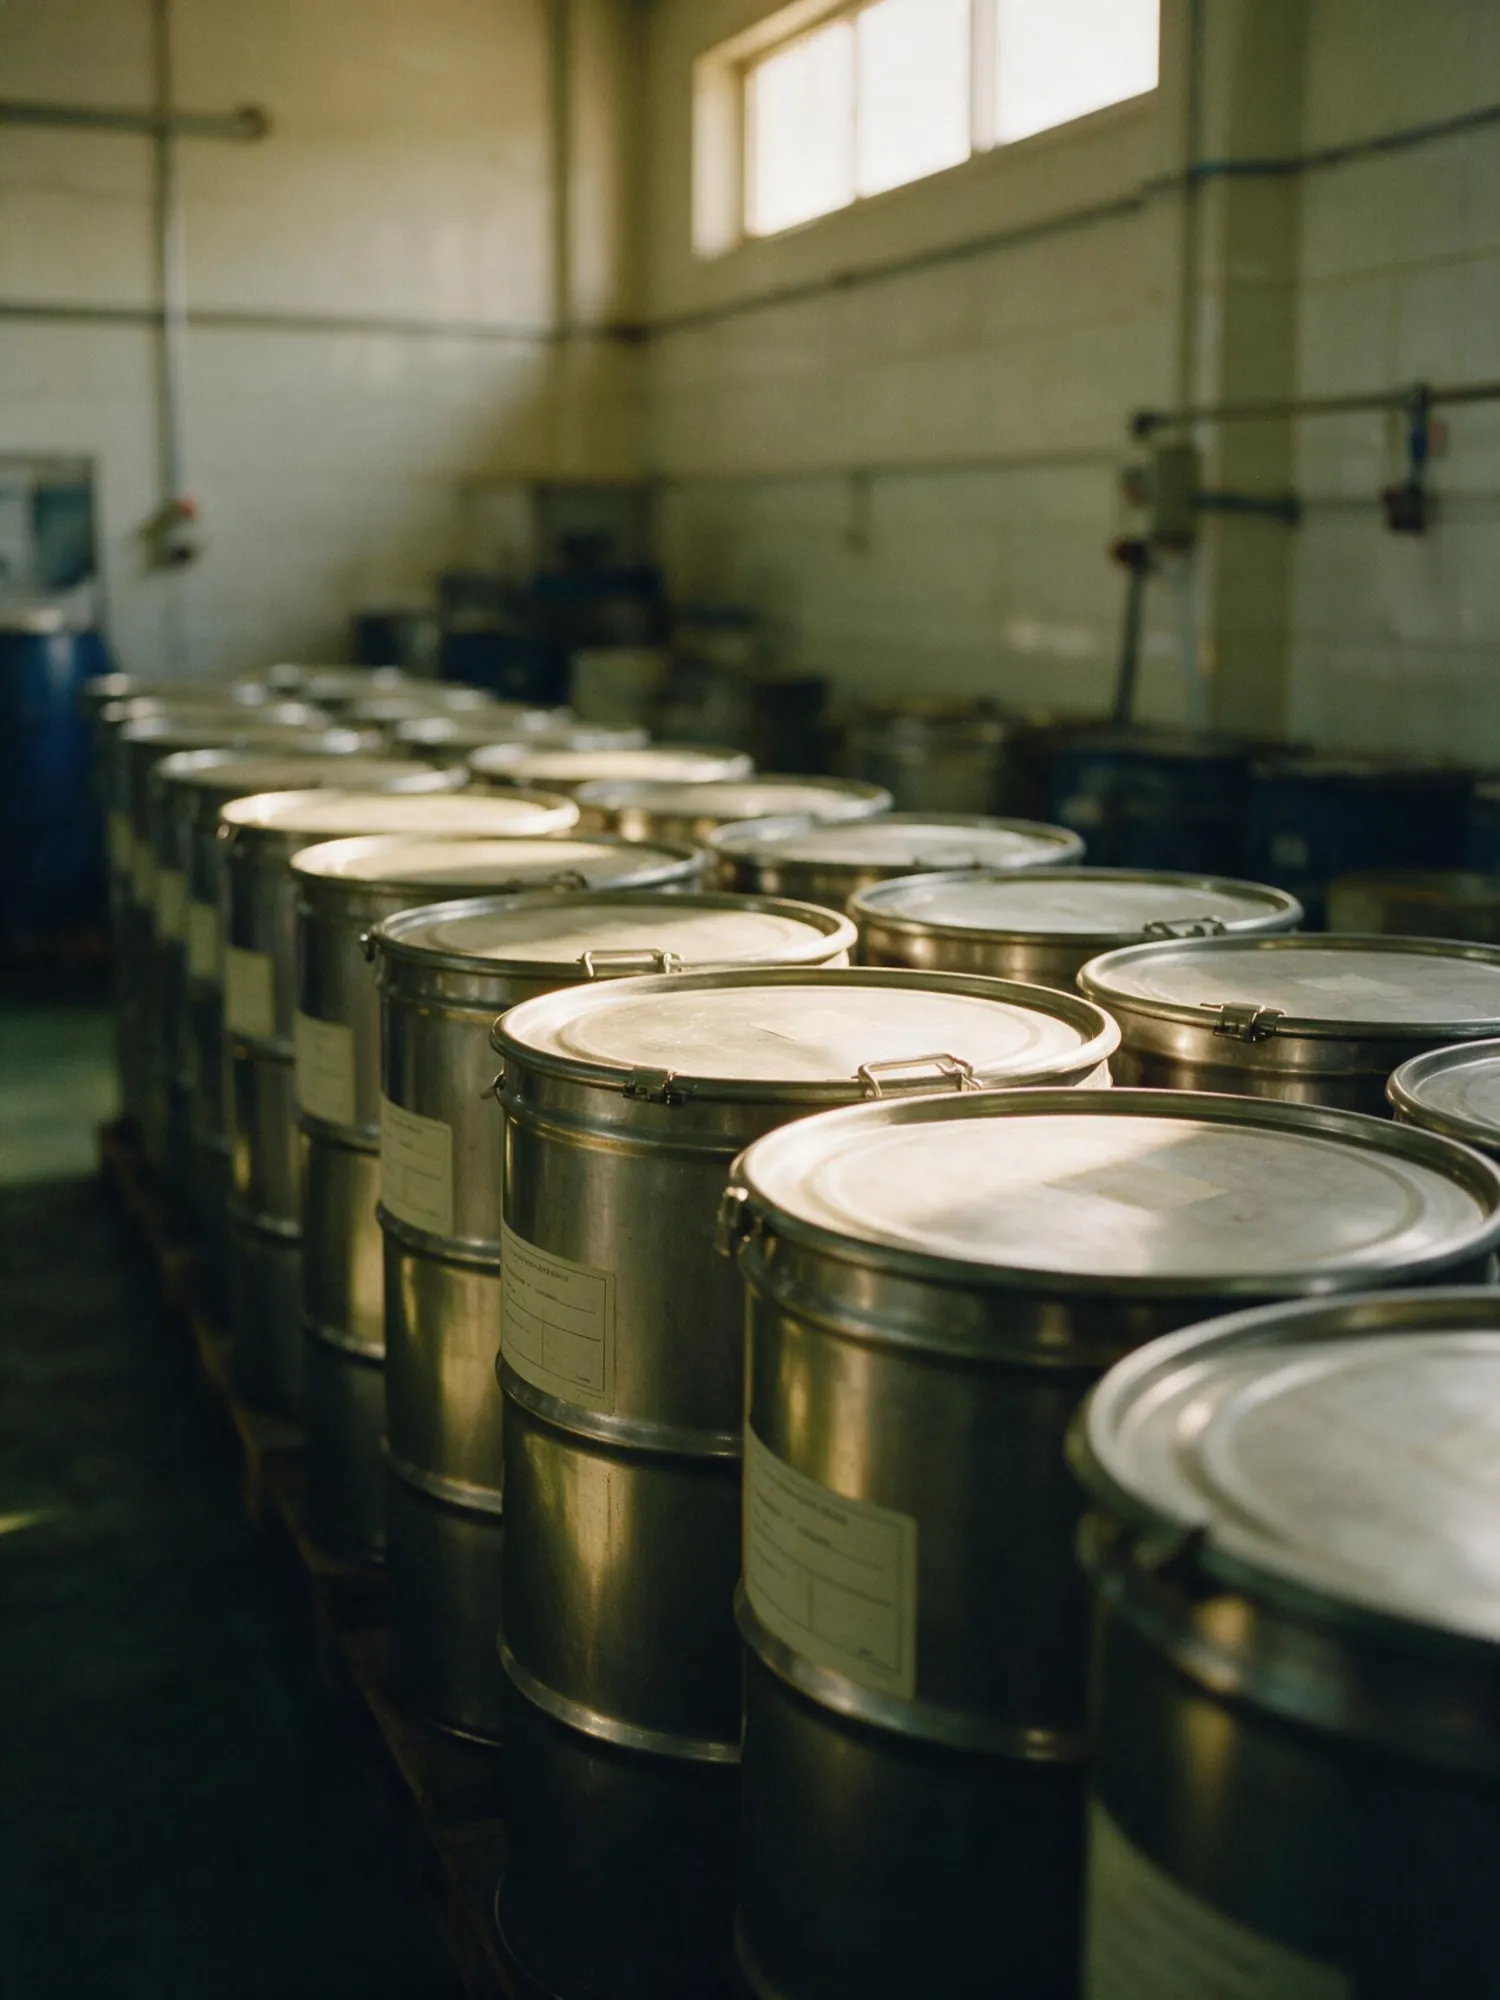
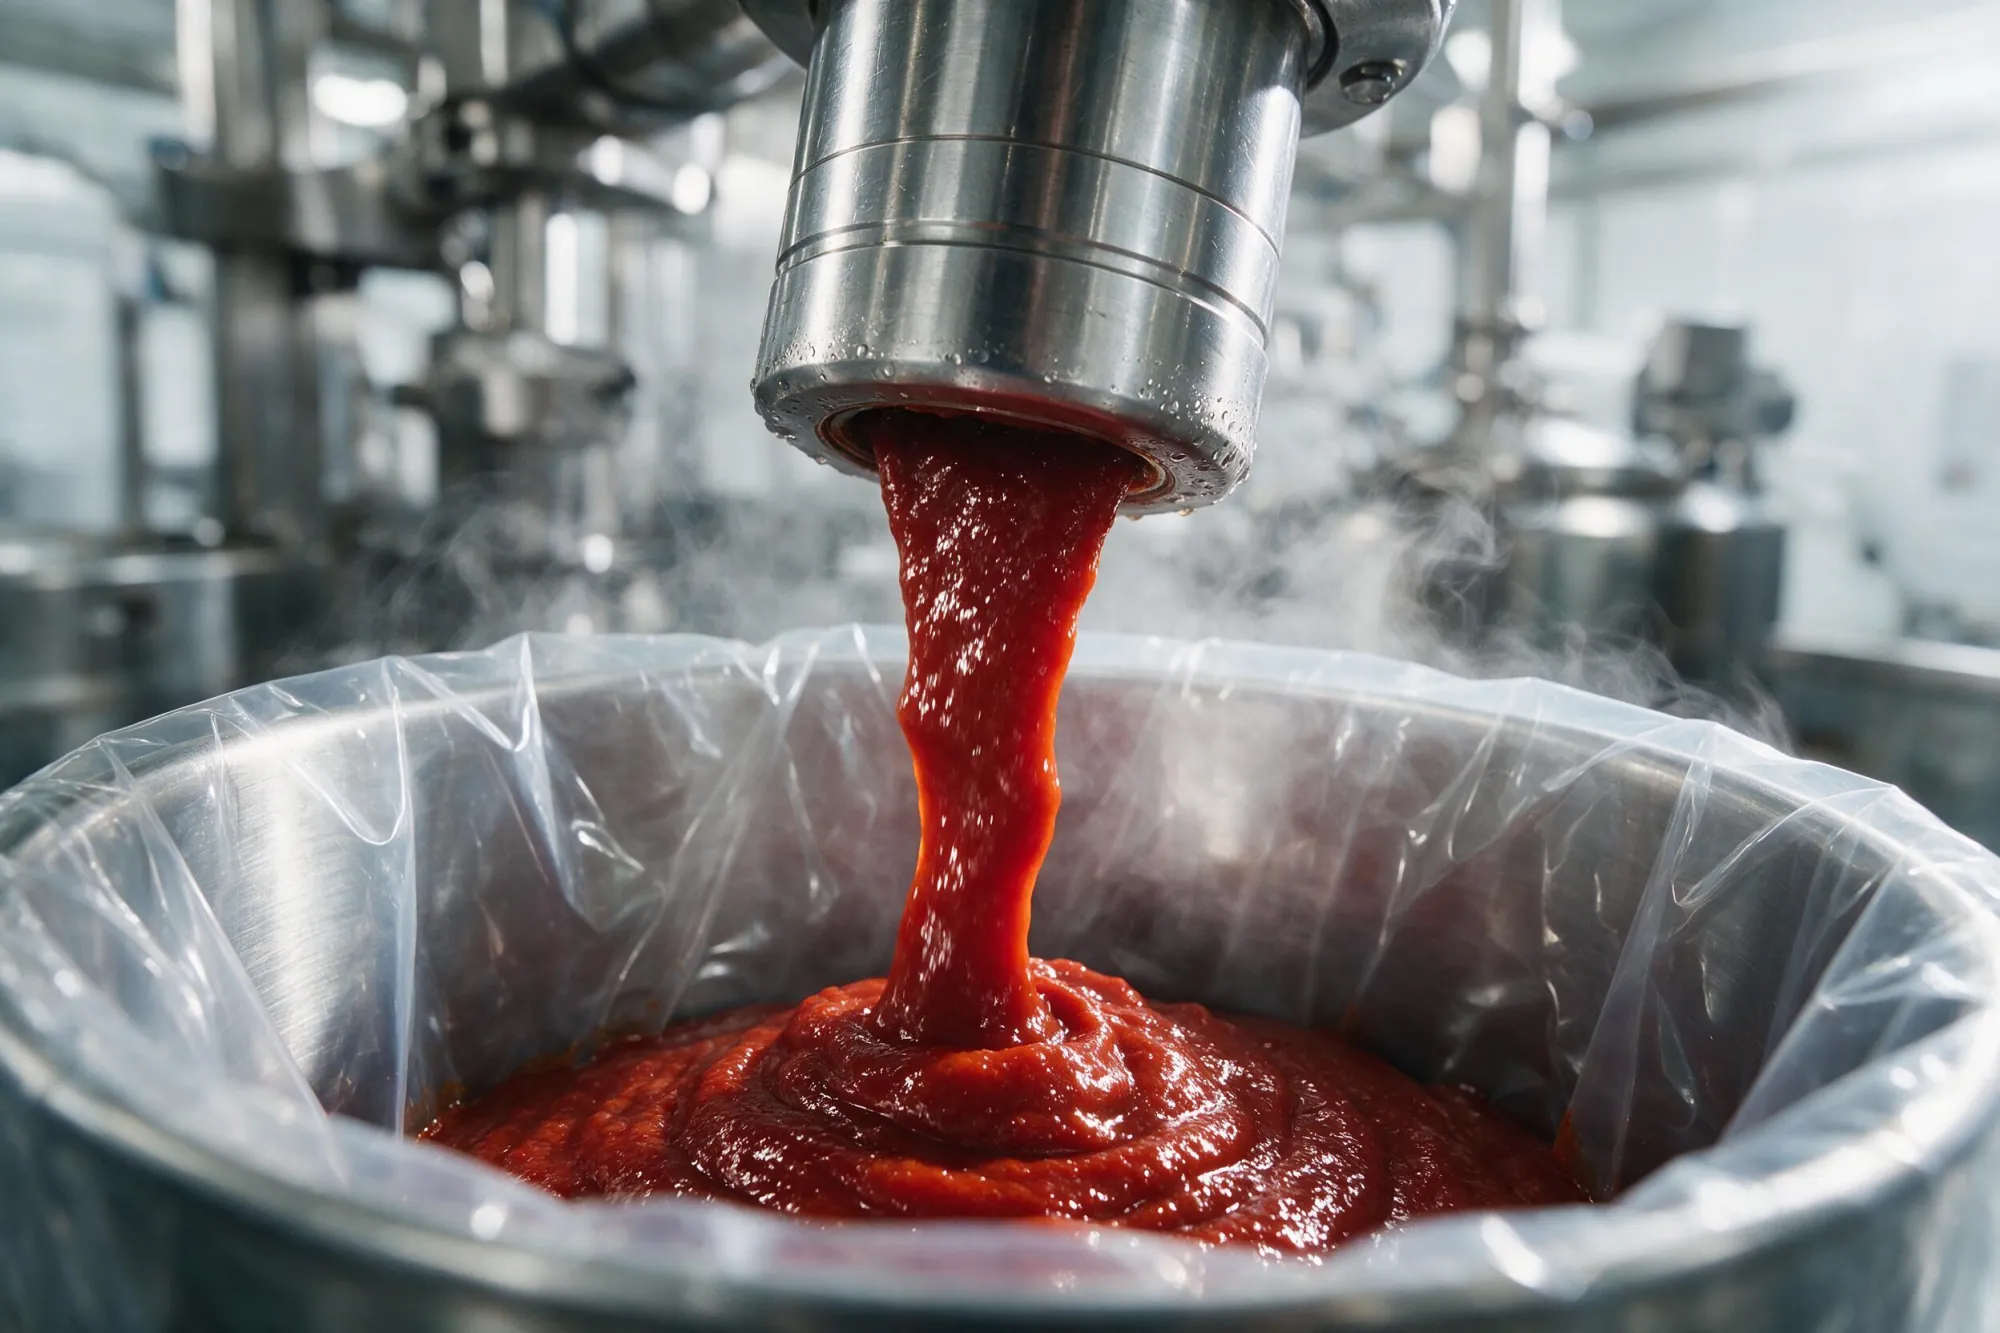
Sealed sterile, at temperature.
The last moment the product meets the air. From here it holds colour, flavour and nutrition for up to twenty-four months with no cold chain and nothing added.